
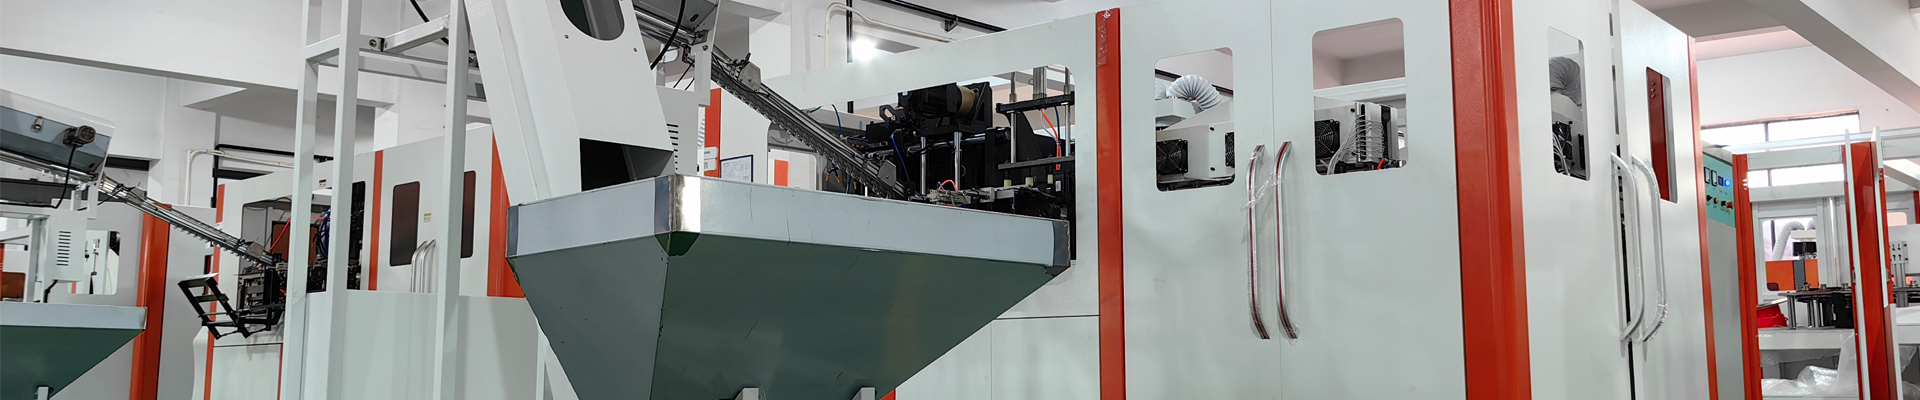
- 1. Building an Export-Oriented PET Bottle Factory: The Opportunity and the Plan
- 2. YuDa Machinery — Your PET Blow Molding Partner
- 3. Site Selection and Workshop Layout for Export Production
- 4. Utility Infrastructure: Water, Electricity, and Compressed Air
- 5. Machine Configuration by Production Scale and Export Target
- 6. Integrating Blow Molding with Filling and Capping (BFC)
- 7. Auxiliary Equipment: Compressor, Chiller, Conveyor, QC Lab
- 8. Export Compliance and Certification Roadmap
- 9. Setting Up the Quality Control Laboratory
- 10. Application Industries for Export PET Bottles
- 11. Service and Support: Open Factory, Free Parts, Commissioning
- 12. Frequently Asked Questions
- Conclusion
Building an Export-Oriented PET Bottle Factory: The Opportunity and the Plan
Global demand for packaged water, carbonated soft drinks, edible oil, and household chemicals keeps pushing beverage brands and private-label distributors to localize bottling close to growing consumption markets. Setting up an export-oriented PET bottle manufacturing factory is no longer reserved for multinational corporations. A well-planned turnkey plant can serve regional export corridors, free-trade zones, and global retail supply chains from a single disciplined production site. The central decision is not whether PET is the right material — its clarity, light weight, impact resistance, and recyclability are well established — but how to configure the factory so it consistently meets the quality, hygiene, and certification expectations of importing markets.
This guide walks an investor or plant manager through the complete setup of an export-grade PET bottle factory: from site selection and workshop layout, through utility design and machine configuration by scale, to blow-fill-cap integration, auxiliary equipment, export compliance, and in-house quality control. The objective is a factory that ships compliant, leak-free, dimensionally stable bottles to customers on multiple continents without rework or border rejection.
A successful export plant shares five non-negotiable traits. First, the blow molding equipment must deliver repeatable bottle weight and wall distribution so every export carton meets the same specification. Second, the production flow must protect bottles from contamination between blowing and capping. Third, the utility backbone — stable power, clean water, and reliable compressed air — must be engineered, not improvised. Fourth, the documentation package must satisfy the food-contact and machinery-safety rules of each destination. Fifth, the team must run a disciplined QC laboratory rather than rely on visual inspection alone. The sections below build these traits into a concrete plan.
Throughout this guide we reference the PET bottle blow molding machines built by YuDa Machinery, a Wanplas factory, because the same engineering principles apply whether you buy a single semi-automatic molder or a fully integrated blow-fill-cap line. YuDa, a Wanplas factory, brings more than 20 years of experience, exports to 60-plus countries, and holds 20-plus patents in PET blow molding, making it a practical reference point for how a turnkey export line is specified and supported.
YuDa Machinery — Your PET Blow Molding Partner
YuDa, a Wanplas factory, is a top manufacturer of PET bottle blow molding machines in China with more than 20 years of focused experience in stretch blow molding. The factory exports to over 60 countries and ranks among the top two PET blow molding manufacturers in China, supported by 20-plus patents that cover heating, cam linkage, and energy-saving oven design. As part of the Wanplas group, YuDa shares the group’s quality standards, open-factory policy, and the brand-wide commitment to ship reliable, serviceable production lines to B2B bottlers worldwide.
The YuDa product range spans every scale an export plant can need: a high-speed FGX series for high-volume lines, a standard-speed fully automatic series for regional export, a semi-automatic series for pilot and niche output, and two integrated blow-fill-cap platforms — the Linear BFC CombiBlock and the Bottle BFC machine. Choosing among them is the single most important configuration decision in the whole project, and it is addressed in detail in the selection section below.
FGX High Speed PET Blow Molding Machine
The FGX High Speed series is engineered for high-volume export production where bottle cost per thousand and line uptime decide margin. Its defining advantage is a minimized heater pitch of 38.1 millimeters, which concentrates infrared energy on the preform and cuts electricity consumption by more than 30 percent compared with conventional heating ovens. A unique cam linking system integrates mold opening, mold locking, and bottom-mold elevating into one synchronized movement, while a high-speed servo driving system sustains single-mode speeds of 2,500 to 3,000 BPH that scale to 8,000 to 15,000 BPH across multiple cavities.
| Parameter | FGX High Speed Series |
|---|---|
| Output range | 8,000 to 15,000 BPH |
| Mold cavities | 6 to 12 cavities |
| Bottle volume range | 0.2 to 2.0 liters |
| Single-mode speed | 2,500 to 3,000 BPH per mold |
| Heater pitch | 38.1 mm (energy-saving layout) |
| Energy saving | 30%+ versus conventional oven |
| Drive system | Servo cam linking, high-speed |
| Monitoring | Remote PLC data monitoring |
| Cost level | High |
Standard Speed Fully Automatic PET Blow Molding Machine
The Standard Speed series covers the broad middle of the export market: regional brands, contract bottlers, and private-label suppliers that need full automation without the premium of a high-speed line. It uses an advanced heating system and energy-saving technologies to keep preform scrap and power draw in check, and its modular design makes mold changeovers and maintenance cost-effective. For most Medium-tier exporters this is the balanced workhorse.
| Parameter | Standard Speed Series |
|---|---|
| Output range | 1,000 to 7,000 BPH |
| Mold cavities | 2 to 8 cavities |
| Bottle volume range | 0.2 to 2.0 liters |
| Heating system | Advanced infrared oven |
| Energy technology | Energy-saving heating control |
| Automation | Full automatic, continuous |
| Modularity | Modular for fast changeover |
| Cost level | Medium |
Semi-Automatic PET Blow Molding Machine
The Semi-auto series is the entry point for pilot lines, niche export products, and small enterprises testing a new market. Procurement cost sits at the Low tier, and many units are ready to ship, which shortens lead time. Operators load preforms manually, so labor per bottle is higher, but the capital barrier is the lowest in the YuDa range.
| Parameter | Semi-Auto Series |
|---|---|
| Output range | 800 to 2,000 BPH |
| Mold cavities | 2 to 4 cavities |
| Bottle volume range | 0.2 to 2.0 liters |
| Loading | Manual preform loading |
| Best fit | Small enterprises, pilot export |
| Availability | Ready to ship |
| Cost level | Low |
Linear BFC CombiBlock and Bottle BFC Machine
The two integrated platforms remove the empty-bottle conveyor entirely. The Linear BFC CombiBlock is a compact, simple, easy-to-operate mini linear blow-fill-cap unit that saves plant area — a strong fit where floor space is expensive or the export volume is concentrated in one bottle size. The Bottle BFC machine produces PET bottles while filling drinking water and installs the caps in one continuous process, which is the most hygienic configuration for export food and beverage because the finished bottle is never exposed as an empty container.
| Feature | Linear BFC CombiBlock | Bottle BFC Machine |
|---|---|---|
| Process integration | Blow + fill + cap, linear | Blow + fill + cap, one process |
| Footprint | Saves plant area, compact | Enclosed, minimal empty-bottle path |
| Operation | Simple, easy to operate | Automated capping inline |
| Typical product | Water, edible oil, detergent | Drinking water bottling |
| Cost level | Very High | Premium |
Site Selection and Workshop Layout for Export Production
The factory layout determines whether your export line runs clean, fast, and auditable. A poor layout creates long empty-bottle conveyors, cross-traffic between raw preforms and finished cartons, and cramped maintenance access that extends downtime. A good layout separates flow into a clean one-way path: preform intake, conditioning and heating, stretch blow, fill and cap, inspection, packing, and finished-goods storage, with utilities and the QC lab placed for short service runs.
For an export plant, the single most important layout principle is contamination control between blowing and capping. Whenever the blow molder and filler are separate machines, the empty bottles travel on a conveyor and must pass through an enclosed, filtered clean tunnel. Whenever they are combined in a BFC CombiBlock, that conveyor disappears and the hygiene risk drops sharply. Choose the integrated layout when the export market demands the strictest food-hygiene documentation.
Space requirements scale with the line. A Low-tier semi-auto cell fits in 400 to 600 square meters including preform storage and packing. A Medium-tier standard-speed line needs 800 to 1,200 square meters. A High or Very High tier built on the FGX series or a Linear BFC CombiBlock needs 1,500 to 2,500 square meters to hold preform silos or gaylord racks, the blowing hall, filling and capping, a packing zone, a QC lab, and a finished-goods warehouse sized for export lead times.
| Flow stage | Process activity | Primary equipment | Layout note |
|---|---|---|---|
| 1. Intake | Preform receiving and storage | Preform racks, dryer | Climate-controlled, off the floor |
| 2. Conditioning | Preform heating | Infrared oven, 38.1 mm pitch | Stable ambient, vented heat |
| 3. Blow | Stretch blow molding | FGX / Standard / Semi-auto | One-way flow, service aisle |
| 4. Air recovery | Low-pressure reclaim | Air recovery tank | Near blow molder |
| 5. Fill | Liquid filling | Filler (BFC or standalone) | Enclosed clean zone |
| 6. Cap | Capping | Capper (inline) | Directly after filler |
| 7. Inspect | QC and reject | QC lab, check weigher | Sampled off the line |
| 8. Pack | Packing and palletizing | Conveyor, packer, wrapper | To finished-goods warehouse |
Design the workshop with a concrete or epoxy floor that drains and cleans easily, a ceiling height of at least 4.5 meters to clear oven exhaust and overhead conveyors, and separate personnel and material doors to keep traffic one-directional. Reserve a dedicated room for the QC laboratory with controlled temperature, because bottle weight and top-load results drift with ambient humidity. Place the compressor and chiller in a separate plant room so heat and noise stay out of the bottling hall.
Preform specification belongs in the layout conversation because it drives storage and conditioning space. Export bottles are blown from injection-molded PET preforms whose neck finish, color, and gram weight are fixed at the injection stage. If you buy preforms from a qualified supplier, you need a climate-controlled preform warehouse and a loader; if you inject preforms in-house, you add an injection molding cell and a crystallizing dryer to the floor plan. Either way, keep preforms off the floor on racks and protect them from dust, because a contaminated preform becomes a rejected bottle two stations later. The 38.1-millimeter heater pitch on YuDa ovens means the conditioning zone is compact, but it still needs stable ambient air so the infrared lamps reach a repeatable preform temperature before the stretch rod enters.
Traffic separation is the last layout discipline export auditors look for. Raw preforms and finished cartons must never share a path, and personnel moving between the warehouse and the bottling hall should cross a hygiene gate. A simple one-way colored floor line, with signs in the local language and the export destination language, prevents the cross-contamination that empty-bottle conveyors invite. Document the flow on the layout drawing and keep that drawing in the same file as the compliance records, because a customer audit will ask to see it.
Utility Infrastructure: Water, Electricity, and Compressed Air
Utility design is where many first-time export plants under-spend and later regret it. A PET blow molding line is sensitive to power quality, needs clean process water for cooling and rinsing, and consumes compressed air in two distinct pressure classes. Engineer each utility to a named capacity tier rather than guessing from nameplate power.
Electricity must arrive through a stable three-phase supply with voltage tolerance matched to the equipment (commonly 380 to 480 V depending on destination standards) and protected by surge suppression, because a servo-driven blow molder reacts badly to sags. Size the incoming supply for the full connected load plus the compressor and chiller, not just the molder. Plan a backup generator or UPS for the control system so a power dip does not scrap a preform batch inside the oven.
Water serves two purposes. Process cooling water circulates through the chiller to the oven lamps and molds, and it must be filtered and, in hard-water regions, treated to avoid scale that insulates heat exchangers. Rinse water for bottles and caps must meet the same hygiene standard as the product contact surface, typically filtered and sanitized. Estimate water volume from line speed and chiller duty; in hot climates the chiller itself becomes the largest cooling load.
Compressed air is the most misunderstood utility in blow molding. Stretch blow uses high-pressure air, often in the range needed to stretch and blow the preform against the mold, plus low-pressure air for mold cooling, valve actuation, and pneumatic handling. A High-tier FGX line therefore needs a dedicated high-pressure compressor, a low-pressure receiver, and an air-recovery tank that captures the exhaust from the blow stroke and reuses it for cooling. Without recovery, energy cost per bottle rises noticeably, which hurts export margin.
Analyze the air balance before you size the compressor, because the recovery tank changes the math. The stretch-blow stroke vents a large volume of high-pressure air the instant the bottle is formed; capturing and stepping that air down to low pressure for mold cooling recovers energy that a once-through system throws away. Size the high-pressure compressor to the blow demand of the chosen cavity count, then size the recovery and low-pressure loop to cover cooling and valves. A correctly balanced air plant can move a Medium or High tier line from the High energy bracket toward the Medium bracket per bottle, which compounds across millions of export units per year.
Electrical protection deserves the same analysis. Servo-driven blow molders and fillers react to voltage sag within a cycle, and a sag during the oven dwell can scorch a preform batch. Install surge suppression at the incoming panel, isolate the control transformers, and provide a UPS for the PLC and HMI so a brief outage does not lose a recipe or desynchronize the cam linkage. For export plants in regions with unstable grids, a backup generator that starts on transfer keeps the line from a cold restart that wastes preforms and production time.
| Utility | Function in PET plant | Design recommendation | Cost sensitivity |
|---|---|---|---|
| Electricity | Drive ovens, servo, filler, capper | 3-phase, surge protected, sized to full load | Medium |
| Process water | Chiller loop, mold cooling | Filtered, treated in hard-water areas | Low |
| Rinse water | Bottle and cap hygiene | Filtered, sanitized to contact standard | Medium |
| High-pressure air | Stretch-blow stroke | Dedicated HP compressor + receiver | High |
| Low-pressure air | Cooling, valves, handling | Receiver + air recovery tank | Medium |
Machine Configuration by Production Scale and Export Target
The correct machine configuration follows directly from your export target volume and the number of bottle sizes you must support. A plant serving one export customer with a single water bottle should choose an integrated line for hygiene and floor savings. A plant serving many SKUs across regional export markets should choose a flexible standard-speed or high-speed blow molder with quick-change molds. The table below maps export target volume to a recommended YuDa line, cavity count, output, and relative cost level.
| Export target volume (scale tier) | Recommended YuDa line | Cavities | Output (BPH) | Cost level |
|---|---|---|---|---|
| Low — pilot or niche export | Semi-auto + separate filler | 2 to 4 | 800 to 2,000 | Low |
| Medium — regional export | Standard Speed fully automatic | 2 to 8 | 1,000 to 7,000 | Medium |
| High — national plus export | FGX High Speed series | 6 to 12 | 8,000 to 15,000 | High |
| Very High — multi-market export | Linear BFC CombiBlock | Integrated | 8,000 to 15,000 | Very High |
| Premium — global brand OEM | Bottle BFC full line | Integrated | Up to 15,000 | Premium |
When the export target is a single high-volume SKU such as a 500-milliliter water bottle, the FGX High Speed series at 8,000 to 15,000 BPH delivers the lowest bottle cost. When the target spans several bottle sizes and moderate volumes, the Standard Speed series at 1,000 to 7,000 BPH with modular molds is more capital-efficient. When the brief is the strictest hygiene documentation for food and beverage export, step up to the Linear BFC CombiBlock or Bottle BFC machine so the empty bottle never exists as a separate handled object.
Remember that output in BPH is a nameplate figure. Real export throughput depends on preform feed consistency, oven conditioning, mold cooling, filler speed, and cap feeding. Build the line around the bottleneck, not the highest number on a brochure. A YuDa engineer will model the whole line during configuration so the blow molder, filler, and capper are balanced and no single station forces the others to idle.
Integrating Blow Molding with Filling and Capping (BFC)
Blow-fill-cap integration is the architectural choice that most improves export hygiene and floor efficiency. In a conventional two-step plant, preforms are blown into empty bottles, the bottles travel on a conveyor, and only later are they filled and capped. Each meter of empty-bottle conveyor is a meter where dust, insects, or condensation can reach the inside surface. In a BFC CombiBlock the bottle is blown, filled, and capped inside one enclosed frame, so the empty bottle essentially does not exist as a handled product.
YuDa offers two BFC approaches. The Linear BFC CombiBlock is a compact, simple, easy-to-operate mini linear unit that specializes in saving plant area — ideal when the export volume concentrates in one or two bottle sizes and real estate is costly. The Bottle BFC machine produces PET bottles while filling drinking water and installs the caps in one process, which is the most contained configuration for drinking-water export. Both options reduce the clean-room volume, lower airborne-contamination risk, and cut utility consumption compared with a separated blow-plus-fill layout.
Integration also changes the utility plan. Because the blow and fill stations share a frame, the compressor, chiller, and electrical supply are consolidated, and the air-recovery loop is shorter. Maintenance becomes centralized at one machine rather than two, which simplifies spare-parts planning and technician training. For an export plant that must pass a customer audit, a single integrated, documented, monitored machine is easier to defend than two separate lines with a conveyor bridge between them.
The trade-off is flexibility. A dedicated blow molder plus a separate filler lets you run different bottle sizes on the molder while keeping one filler, and it is simpler to expand blowing capacity independently of filling. Choose separation when SKU variety is high and volumes are moderate; choose integration when volume and hygiene dominate. Either way, YuDa configures the line so the blow, fill, and cap stations are speed-matched.
Commissioning an integrated BFC line rewards disciplined planning. Because blowing, filling, and capping share one frame, the calibration sequence matters: the oven conditioning and stretch ratio are set first to lock bottle weight and wall distribution, then the filler timing is matched to the blown bottle’s neck and base, and finally the capper torque is verified so caps seat without stripping. Run this sequence on the customer’s actual preform and cap at the factory acceptance test, not on a substitute, because neck geometry varies by supplier. A YuDa engineer documents the full parameter set during commissioning so your operators can reproduce it on every shift and every export order.
The air-recovery loop inside a CombiBlock is shorter than in a separated layout, which is why integrated lines report lower utility cost per bottle. The recovered blow air feeds mold cooling directly, the low-pressure receiver stays smaller, and the clean-room volume shrinks because the empty bottle never travels. For an export plant bidding on a private-label contract with tight per-bottle cost targets, that utility saving is often the deciding factor between a separated line and a BFC CombiBlock, even before the hygiene argument is counted.
Auxiliary Equipment: Compressor, Chiller, Conveyor, QC Lab
A PET bottle factory is more than a blow molder. The auxiliary equipment decides whether the main machine reaches its nameplate output and whether the bottles are consistent enough to export. Budget for these items explicitly; omitting them is the most common cause of a line that blows good samples but cannot hold spec in a 24-hour export run.
The air compressor was covered under utilities, but it deserves emphasis as a capacity decision: size the high-pressure compressor to the blow stroke of the chosen cavity count, add a low-pressure receiver for cooling and valves, and include an air-recovery tank. Oversizing the compressor wastes energy; undersizing it caps output below the molder’s rating.
The industrial water chiller holds the oven lamps and molds at the temperature that stabilizes bottle weight and wall distribution. In warm climates the chiller duty rises, so select the chiller from the High or Very High cooling tier rather than the minimum. A chiller with a buffer tank smooths load spikes when cavities index.
The conveyor connects blowing to filling when the line is not integrated, and it connects filling to packing in every layout. Specify a clean, enclosed conveyor for the empty-bottle section, with side guides sized to the bottle and a reject gate that diverts fallen or deformed bottles before they reach the filler. After capping, a check weigher and a metal detector or vision system sample the flow.
The QC laboratory is the final auxiliary and the one export customers inspect hardest. It needs a pressure-decay leak tester, a top-load compression rig, a precision balance for bottle weight, and space for burst and wall-thickness checks. Locate the lab in a temperature-controlled room sampled off the line, not in the noisy bottling hall, so measurements are repeatable.
| Auxiliary item | Role | Selection rule | Cost level |
|---|---|---|---|
| High-pressure compressor | Stretch-blow air | Match cavity blow demand | High |
| Low-pressure receiver | Cooling and valves | Plus air recovery tank | Medium |
| Water chiller | Oven and mold cooling | Size to climate and speed | Medium |
| Conveyor | Transport and reject | Enclosed for empty bottles | Low |
| QC laboratory | Leak, top-load, weight | Temperature-controlled room | Medium |
Export Compliance and Certification Roadmap
Compliance is what turns a working bottling line into an export business. The certification set depends on the destination, but a disciplined plant builds the documentation stack once and extends it per market. The standards below are named as plain-text references; this guide does not link to external bodies, and all requirements should be confirmed against the current rules of each importing authority before shipment.
ISO 9001 is the foundational quality-management certification that most export buyers ask for first. It proves the factory controls its processes, records its tests, and corrects deviations. CE marking applies to the production machinery placed on the European market and confirms that the blow molder, filler, and capper meet machinery-safety requirements; it is a property of the equipment and its documentation, not the bottle. FDA food-contact compliance matters for bottles and caps exported to the United States, where the polymer and any additives must meet food-contact material rules. ISO 22000 supports food-safety management for the filled product and is increasingly requested by global retailers and brand owners. Local food-contact regulations of each importing country — such as EU 10/2011 in Europe or equivalent national rules elsewhere — define the specific migration and additive limits the bottle must satisfy.
Compliance rule of thumb: certify the management system (ISO 9001), certify the machine safety (CE where required), certify the material contact status (FDA, EU 10/2011, or local food-contact rules), and certify the food safety chain (ISO 22000 for filled product). Build the file once, then extend per destination.
| Market scope | Standard (plain text) | What it covers |
|---|---|---|
| Global | ISO 9001 | Quality management system |
| European machinery | CE | Machinery safety of equipment |
| United States contact | FDA | Food-contact material rules |
| Filled product safety | ISO 22000 | Food safety management |
| Per destination | Local food-contact regs | National migration and additive limits |
Cost levels for compliance work sit at the Medium to High tier: audits, documentation, and sometimes material requalification add expense but are unavoidable for export. Plan compliance from day one, because retrofitting records and training after the line is running is slower and more expensive than building the system during commissioning. YuDa, as a Wanplas factory, supplies the equipment-side documentation needed for CE and supports customers with the technical files that export audits expect.
Setting Up the Quality Control Laboratory
An export PET bottle lives or dies by its QC record. Visual inspection catches gross defects but cannot prove leak tightness, stack strength, or weight consistency. The QC laboratory must run instrumented tests on every production shift and keep the results traceable to batch and mold cavity.
The leak test uses pressure decay: a finished bottle is sealed, pressurized, and monitored for pressure drop over a fixed time. Any decay above the acceptance limit is a reject, because a leaking bottle fails at the filler or on the shelf. The top-load test compresses the bottle between plates to a defined force and measures deformation or collapse; it confirms the bottle will survive pallet stacking in a container during export transit. The bottle-weight check weighs the finished bottle against the gram-weight tolerance set by the preform and mold design; drift here signals oven conditioning or stretch-ratio problems before they become customer complaints.
Extend the lab with a burst-pressure test for carbonated applications, a wall-thickness or section-weight check to verify material distribution, and a fill-height check after capping to confirm the filler delivers the labeled volume. Record every result with the timestamp, line, and cavity so a customer audit can trace any rejected carton back to its cause.
| Test | Method | Acceptance criterion |
|---|---|---|
| Leak test | Pressure decay | No pressure drop beyond limit |
| Top-load | Compression to defined force | No collapse below min load |
| Bottle weight | Precision weighing | Within gram-weight tolerance |
| Burst pressure | Pressurize to failure (CSD) | Above rated burst |
| Fill height | Post-cap measurement | Matches labeled volume |
Application Industries for Export PET Bottles
A PET bottle factory serves a wide band of export industries, and naming them helps you size the line and choose the right bottle spec. The most common export applications built on YuDa blow molding technology are drinking water, carbonated soft drinks, edible oil, and liquid food; daily-chemical products such as detergent, shampoo, and conditioner; and household and industrial liquids that value the bottle’s light weight and impact resistance for long shipping routes.
For food and beverage export, the bottle must satisfy food-contact rules and usually ISO 22000 for the filled product, and it must hold carbonation pressure where applicable. For daily-chemical export, the priority is chemical resistance and dose-cap compatibility rather than carbonation, but the same blow molding principles apply. For edible oil, the bottle must resist oil migration and hold shape at warm storage temperatures, which calls for careful preform grade selection and wall distribution. Across all of these, the YuDa range — from Semi-auto pilot lines to FGX High Speed and BFC integrated lines — covers the full output span an export supplier needs.
When you specify the factory, list the target industries and their bottle sizes up front. A plant aimed at export drinking water will standardize on one or two bottles and favor BFC integration. A plant aimed at daily-chemical export will run more SKUs and favor a flexible standard-speed or high-speed molder with quick-change molds. The application mix is the bridge between the selection table in section five and the compliance plan in section eight.
Service and Support: Open Factory, Free Parts, Commissioning
Setting up an export plant is a project, not a purchase, and the supplier’s support decides how fast you reach compliant output. As a Wanplas factory, YuDa backs every line with the group’s shared service promises. Before shipment, each machine is tested at the factory so the customer receives a proven configuration rather than a commissioning experiment. YuDa engineers travel for on-site installation and commissioning, train operators, and remain reachable through remote monitoring that reads PLC data from China so abnormalities are flagged early.
The spare-parts policy is the group-wide commitment of USD 500 free parts per year, complemented by free replacement of damaged parts within the warranty. Customers are welcome under the open-factory policy to visit YuDa before ordering, audit the workshop, and run a sample trial on the actual line configuration they plan to buy. For an export investor, that visit is also the moment to confirm the equipment-side documentation needed for CE and for the food-contact files your buyers will request.
Support also covers the softer parts of going export: layout review, utility sizing advice, and training materials in the language of your team. Because the Wanplas group runs multiple specialized factories, adjacent capabilities such as filling lines are coordinated under the Wanplas brand so your project stays single-point accountable even when the scope grows beyond blowing.
Frequently Asked Questions
What is the minimum factory area needed for an export-oriented PET bottle plant?
A pilot Low-tier line with a semi-automatic blow molder and a separate filler can operate in roughly 400 to 600 square meters. A Medium-tier standard-speed automatic line needs about 800 to 1,200 square meters, while a High or Very High tier built around the FGX High Speed series or a Linear BFC CombiBlock requires 1,500 to 2,500 square meters to allow for preform storage, blowing, filling, packing, and a QC laboratory.
Which YuDa line should I choose for regional export volumes?
For regional export and Medium-tier output of 1,000 to 7,000 BPH, the YuDa Standard Speed fully automatic PET blow molding machine is the balanced choice. It pairs an advanced heating system and energy-saving technology with a procurement cost level of Medium, which protects margin for mid-size exporters.
Why integrate blowing and filling in a BFC CombiBlock?
A blow-fill-cap CombiBlock produces the PET bottle and fills plus caps it in one enclosed process. This removes the empty-bottle conveyor, shrinks the clean-room footprint, lowers the risk of airborne contamination, and reduces utility consumption. YuDa offers both the compact Linear BFC CombiBlock and the Bottle BFC machine for this integration.
What certifications do I need to export PET bottles for food and beverage?
At minimum you should hold ISO 9001 for quality management, CE marking for machinery safety on the production equipment, and meet the food-contact requirements of your destination market such as FDA in the United States, EU 10/2011 in Europe, or the local food-contact regulations of each importing country. ISO 22000 supports food safety management for the filled product. All certification names remain plain-text references in this guide.
How much compressed air and cooling does a PET blow line consume?
Stretch blow molding uses high-pressure air for the stretch-blow stroke and low-pressure air for mold cooling and valve actuation. A High-tier FGX line typically needs a dedicated high-pressure compressor plus a low-pressure receiver and an air-recovery tank. Process cooling is handled by an industrial water chiller sized to the oven and mold load; the exact capacity tier depends on ambient climate and line speed.
What quality tests must an export PET bottle pass?
Every export batch should pass a pressure-decay leak test, a top-load compression test to confirm stack resistance, and a bottle-weight check against the gram-weight tolerance of the preform and mold design. Additional checks include burst pressure, fill-height consistency after capping, and visual inspection for gate defects and wall-thickness uniformity.
Can YuDa support installation and commissioning outside China?
Yes. As a Wanplas factory, YuDa provides engineers for on-site installation and commissioning, pre-shipment factory testing, operator training, remote monitoring of PLC data, and the group-wide policy of USD 500 free parts per year plus warranty replacement. Customers are also welcome to visit the open factory before ordering.
Conclusion
Setting up an export-oriented PET bottle manufacturing factory is a disciplined sequence: choose the right YuDa blow molding line for your export volume, lay out a one-way clean flow, engineer power, water, and compressed air to a named capacity tier, integrate blow and fill where hygiene demands it, fund the auxiliary equipment and QC lab, and build the compliance file before the first shipment. The reward is a plant that ships consistent, leak-free, certified bottles to multiple markets without border rejection.
For pilot and niche export, the YuDa Semi-auto series at the Low cost tier is the fastest entry. For regional export, the Standard Speed fully automatic line at the Medium tier balances output and capital. For high-volume export, the FGX High Speed series delivers 8,000 to 15,000 BPH with 30-plus percent oven energy savings. For the strictest hygiene and floor efficiency, the Linear BFC CombiBlock or Bottle BFC machine integrate the whole process in one frame. YuDa, a Wanplas factory, supports each choice with pre-shipment testing, on-site commissioning, the open-factory policy, and USD 500 free parts per year.
If you are planning an export PET bottle plant, send your target volume, bottle sizes, and destination markets, and YuDa will model a balanced line configuration, review your workshop layout, and invite you to the factory for a sample trial run. The right setup plan is the difference between a line that merely blows bottles and a line that wins export customers.






