
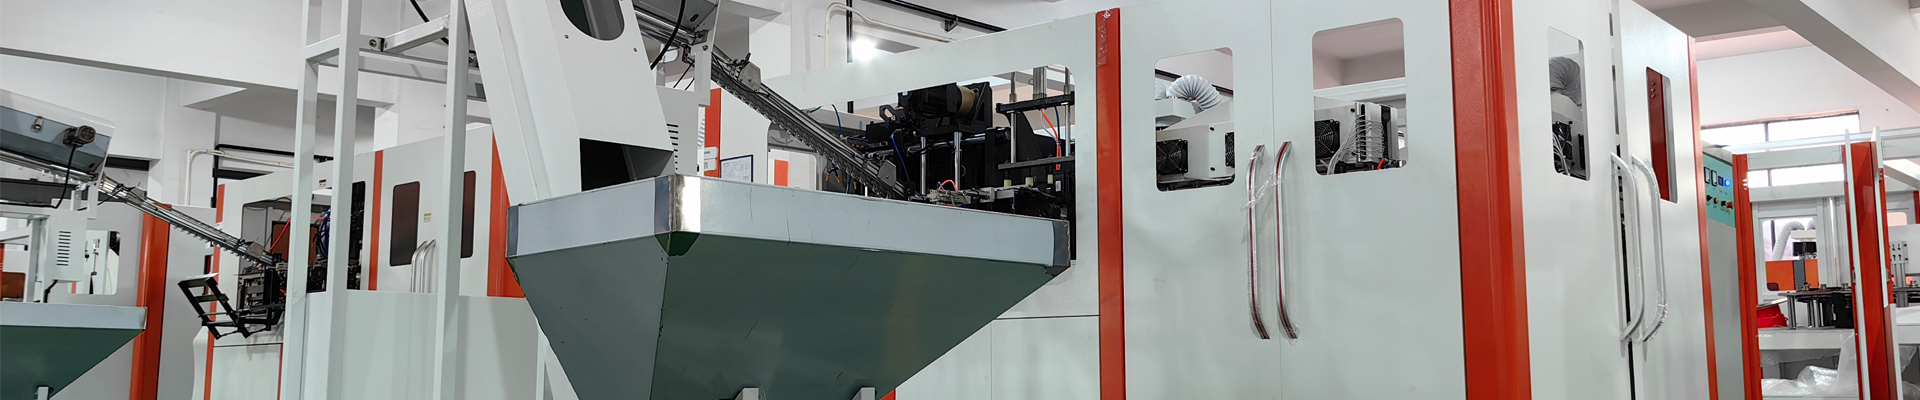
An aging PET bottle blowing production line does not stop earning money overnight, but it quietly drains profit through rising electricity bills, slow cycles, unstable bottle weight, and an ever-growing pile of worn spare parts. For beverage, edible oil, dairy, household care and water bottlers, the question is rarely whether the old line is outdated, but how to modernize it without paying for a complete new line. This guide lays out a low-cost transformation scheme for an old PET bottle blowing production line that targets the five subsystems where dated technology actually costs money: the take-out robot and loading, the infrared heating oven, the servo and drive system, the electrical control, and the blow mold. By upgrading only what is dated and keeping what is still sound, a plant can recover a large share of new-line performance at a fraction of the capital.
YuDa, a Wanplas factory, has spent more than 20 years building PET bottle blow molding machines and now serves customers in 60-plus countries as a top two manufacturer in China with 20-plus patents. The Wanplas group brings together specialized factories across the plastic machinery value chain, and YuDa focuses purely on PET bottle blowing equipment from semi-automatic units for small workshops to high-speed automatic lines for mass beverage production. That focused experience is exactly what an old-line owner needs: practical retrofit knowledge tied to real machine families, not a generic sales pitch. In the sections below we explain each retrofit path, show how project cost breaks into Low, Medium and High tiers using percentage share and payback index points, quantify energy improvement in kWh per 1,000 bottles using relative index points, and introduce the YuDa models that either replace the line or supply the upgraded modules.
The core idea of a low-cost scheme is subtraction before addition. Before buying anything, a plant should measure three numbers on the running line: actual output in bottles per hour, actual electricity in kWh per 1,000 bottles, and reject rate by defect type. Those three measurements become the baseline. Every retrofit option is then judged by how much it moves those three numbers within an acceptable cost tier. This disciplined approach is what separates a transformation that pays back quickly from a scattered list of upgrades that never closes.
Why Old PET Bottle Blowing Lines Become a Cost Burden
Most PET blow lines bought more than eight years ago were designed around asynchronous motors, relay-based control, wide-pitch heating ovens, and manual or pneumatic take-out. Each of those choices was reasonable at the time, yet together they create a performance gap that widens every year as energy prices rise and bottle gram weights fall. The burden shows up in five predictable ways that any plant manager can recognize.
First, electricity consumption per bottle climbs because wide-pitch ovens heat a large volume of air instead of concentrating infrared energy on the preform. A conventional oven can use 30 percent or more excess electricity compared with a compact, closely pitched heating layout. Second, cycle time drifts upward because pneumatic or cam-driven movements lack the precise, repeatable acceleration of a servo system, so the machine cannot safely run at its original rated speed. Third, bottle weight variation grows as heater lamps age unevenly and the control loop cannot compensate, which forces operators to add gram weight as a safety margin and wastes resin. Fourth, unplanned downtime rises because relay logic and analog temperature controllers fail in ways that are hard to diagnose remotely. Fifth, labor cost stays high when a take-out robot is absent and workers must load, transfer and pack by hand.
A ten-year-old PET blow line is rarely worn out at the frame; it is worn out at the controls, the drives and the oven. Those are exactly the parts a low-cost transformation should replace first.
The financial case for transformation is strengthened by the fact that resin and energy are recurring costs, while a retrofit is a one-time spend. A line that saves a few index points of energy every single day, across millions of bottles per year, can justify a Medium or even High tier project on energy savings alone, before counting the labor and reject-rate benefits. The sections that follow turn this logic into a concrete route map.
Transformation Route Overview: Five Upgrade Paths
A complete low-cost transformation scheme for an old PET bottle blowing production line can be organized as five independent upgrade paths. Independence matters: each path can be scoped, budgeted and commissioned on its own, so a plant can phase the work across scheduled maintenance windows instead of freezing the line for a long stoppage. The five paths are take-out robot and automation, infrared heating oven upgrade, servo drive and energy-saving retrofit, electrical control and remote monitoring, and blow mold and bottle lightweighting.
Path one addresses labor and transfer consistency by adding or modernizing the take-out robot and upstream-downstream handling. Path two attacks the largest energy consumer by replacing the oven lamps, reflectors and pitch with a compact high-efficiency heating section. Path three converts the main motions and air systems to servo control for speed and repeatability. Path four replaces the control cabinet with a modern PLC and HMI plus remote monitoring. Path five optimizes the blow mold and bottle design to cut gram weight without losing top-load or drop performance.
| Upgrade Path | Primary Benefit | Typical Cost Tier | Best Phase to Start |
|---|---|---|---|
| Take-out robot and automation | Labor reduction, transfer consistency | Low to Medium | After oven and servo |
| Infrared heating oven upgrade | Energy saving, preform temperature stability | Low to Medium | First |
| Servo drive and energy-saving retrofit | Cycle time, repeatability, power | Low to Medium | First or second |
| Electrical control and remote monitoring | Diagnostics, uptime, data | Medium | With servo |
| Blow mold and bottle lightweighting | Resin saving, gram weight | Medium to High | After base is stable |
The order shown is a recommendation, not a rule. A plant with cheap labor but expensive electricity should lead with the oven and servo. A plant with tight resin margin should lead with the mold and bottle design. The cost tier column already hints at the budgeting logic that section four makes explicit: Low, Medium and High tiers are defined by the share of a comparable new line plus a payback index point.
Path One to Path Five in Detail
Path One: Take-Out Robot and Automation Retrofit
The take-out robot moves finished bottles from the blow station to the conveyor, rejects deformed bottles, and keeps the transfer timing locked to the machine cycle. On older lines this task is manual or handled by a slow pneumatic picker, which caps real output below the rated speed and introduces handling defects. A modern servo take-out robot synchronizes with the mold movement, reduces bottle-to-bottle contact, and frees operators for quality checks instead of physical transfer.
For a low-cost scheme the robot is often mounted on the existing frame using the original transfer pitch, so no new base or foundation is required. The gain is steady rather than spectacular: a small index improvement in effective output and a clear drop in handling rejects. When paired with downstream conveyors and a vision check, the same robot becomes the first building block of a lights-out packaging cell.
Path Two: Infrared Heating Oven Upgrade
The heating oven is the single largest energy user on a PET blow line and the most common source of weight variation. Conventional ovens use a wide lamp pitch, simple reflectors and analog temperature control, so a large share of infrared energy heats the surrounding air instead of the preform. A compact upgrade shortens the lamp pitch, adds high-reflectivity liners, and places each lamp on a closed-loop temperature controller fed by a pyrometer or thermocouple near the preform surface.
YuDa’s energy-saving design philosophy centers on minimizing the heater distance, with a compact 38.1 mm pitch that concentrates infrared energy on the preform and saves more than 30 percent electricity compared with conventional heating ovens. That same principle is what a retrofit oven section should imitate: shorter pitch, better reflection, and per-lamp control. The result is a more uniform preform temperature profile, which then allows the stretch blow process to run at lower gram weight with the same bottle performance.
Path Three: Servo Drive and Energy-Saving Retrofit
The main motions of a PET blow machine are mold-opening, mold-locking and bottom-mold-elevating, plus the stretch and blow sequence. On dated lines these are driven by pneumatic cylinders or asynchronous motors with mechanical cams, which are hard to tune and waste compressed air or electricity. A servo retrofit replaces those with high-response servo motors linked through a cam linking system that integrates mold-opening, mold-locking and bottom-mold-elevating into one synchronized movement.
The benefits are threefold. Speed rises because the servo reaches the next position faster and with less overshoot. Repeatability rises because the motion profile is digital and identical every cycle. Energy falls because the servo draws power only during motion and regenerates during deceleration, unlike a constantly running asynchronous motor. For many older lines this single retrofit recovers the rated speed the machine had when new, which is often the cheapest way to add real bottles per hour.
Path Four: Electrical Control and Remote Monitoring
Relay logic and analog controllers are reliable until they are not, and when they fail the fault is rarely obvious on the floor. A control retrofit replaces the cabinet with a modern PLC and HMI, adds recipe management so product changeovers are a few on-screen steps, and connects the line to a remote monitoring system. YuDa’s monitoring approach lets engineers at the China headquarters check PLC data through a mobile connection and feed abnormal conditions back to the client site, turning a mysterious stoppage into a guided fix.
Remote monitoring also supports the data acquisition a plant needs for continuous improvement. Cycle counts, reject reasons, lamp hours and energy per shift become visible, so the next retrofit decision is based on evidence rather than memory. For a low-cost scheme this path is usually bundled with the servo retrofit because both touch the same cabinet and motion controllers.
Path Five: Blow Mold and Bottle Lightweighting
The blow mold defines the bottle shape, the cooling rate and the final gram weight. An old mold may have conservative wall distribution, poor cooling channels or worn venting, all of which push gram weight upward. A mold retrofit, combined with a redesigned preform and bottle, can cut resin use per bottle while keeping top-load and drop performance within specification. This path is the only one that saves a recurring material cost rather than an energy or labor cost, which is why it matters most for high-volume water and beverage bottlers.
Lightweighting must be done carefully. The preform gate, the stretch ratio and the blow pressure profile all interact, so the mold change should be validated with a short trial run and a top-load and drop test before full production. Because this path depends on a stable oven and servo base, it is best scheduled after paths two and three are complete.
Cost Tiering of Retrofit Projects
To keep a transformation low-cost, every option must be placed in a cost tier. We define three tiers by two numbers: the project cost as a percentage share of a comparable new line, and a payback index point expressed in relative months. The payback index point is a normalized figure, not an absolute calendar promise, because the real payback depends on local energy price, labor rate and bottle volume. What the index gives is a fair comparison between tiers.
| Cost Tier | Scope Included | Cost Share of New Line | Payback Index Point | Risk Level |
|---|---|---|---|---|
| Low | Heating oven upgrade plus servo drive on main motions | 15 to 25 percent | 8 to 14 index points | Low |
| Medium | Low tier plus take-out robot, full control replacement, remote monitoring | 32 to 48 percent | 14 to 22 index points | Medium |
| High | Medium tier plus modular rebuild, new blow molds, bottle redesign, optional BFC integration | 55 to 72 percent | 20 to 30 index points | Medium to High |
The Low tier is the workhorse of a low-cost scheme. It captures the two biggest energy and speed leaks, oven and servo, for a modest share of new-line cost, and because both upgrades are proven on the existing frame the execution risk is low. The Medium tier is the sweet spot for plants that also suffer from labor cost and unexplained downtime, since the robot and monitoring address those directly. The High tier edges close to a new line in spend, but it remains cheaper than a full replacement and preserves the installed foundation, utilities and floor space, which are costs a new line would repeat.
A useful rule for budgeting: if the required capacity gain is within one tier and the frame is sound, retrofit; if the capacity gain crosses more than one tier or the frame fails a safety and hygiene review, buy new. The comparison table in section six makes this trade-off explicit. Owners should also reserve a small contingency, typically a few percent of the project share, for unforeseen items discovered only after the cabinet is opened, such as worn wiring or a degraded compressor. A phased plan that front-loads the Low tier lets the saving from the first phase help fund the later Medium tier, which is often the most practical way to reach a High tier result without a single large approval.
Energy Efficiency Gains: kWh per 1,000 Bottles
Energy is the easiest burden to measure and the easiest gain to bank. We express the result two ways: an absolute reference in kWh per 1,000 bottles, and a relative index point where a ten-year-old conventional line equals 100. Absolute figures vary with bottle gram weight, preform temperature and ambient conditions, so the index point is the fairer way to compare options; the absolute column is a typical reference for a standard 500 ml water bottle on a two-step line.
| Line Condition | kWh per 1,000 Bottles (reference) | Energy Index Point | Typical Cost Tier |
|---|---|---|---|
| Ten-year-old conventional line (baseline) | 9.8 | 100 | Reference |
| After oven upgrade only | 8.2 | 84 | Low |
| Oven plus servo retrofit | 7.1 | 72 | Low |
| Medium tier (add robot, control, monitoring) | 6.5 | 66 | Medium |
| High tier modular rebuild with new molds | 6.0 | 61 | High |
| New YuDa FGX high-speed line | 5.9 | 60 | New |
| New YuDa Standard Speed line | 6.8 | 69 | New |
The table shows why a Low tier retrofit is often enough. Moving from index 100 to 72 already captures roughly two-thirds of the gap to a brand-new high-speed line, at a cost share of only 15 to 25 percent. The last few index points, from 61 down to 60, cost a full new-line purchase, which is rarely justified by energy alone. A plant should therefore treat the energy index as a guide: stop retrofitting when the next tier costs more than the energy it saves, and reserve a new line for when capacity or gram weight must change by a full tier. It is worth noting that the absolute kWh reference assumes a standard 500 ml water bottle on a two-step line; a heavier edible-oil bottle or a carbonated bottle with a stronger base will show higher absolute figures, yet the index relationship between tiers stays consistent because the same oven and servo technology drives both. For this reason the index point is the better planning tool, and the absolute column should be read as a sanity check rather than a promise.
Retrofit Versus New Line: Side-by-Side Comparison
Owners sometimes assume a new line is automatically better, but the right answer depends on the condition of the existing foundation and the size of the performance gap. The table below compares a retrofit (Medium to High tier using existing frame) with a new PET blow molding machine across the factors that matter to a bottling operation.
| Decision Factor | Retrofit (existing frame) | New PET Blow Molding Machine |
|---|---|---|
| Capital cost | Low to Medium (15 to 72 percent of new) | High (full investment) |
| Lead time | Short, phased in maintenance windows | Longer, including foundation and utilities |
| Production downtime | Limited, modular stoppages | Full line changeover |
| Capacity gain | Up to about one tier | One tier or more, by model |
| Energy index point | 61 to 72 | 60 to 69 |
| Floor space and utilities | Reused as built | May need redesign |
| Warranty and support | Covered by retrofit scope | Full new-machine warranty |
| Best when | Frame sound, gap within one tier | Capacity or gram weight must jump a tier |
The comparison is deliberately technology-versus-technology, not brand-versus-brand. A retrofit wins on capital, lead time and downtime; a new machine wins on capacity headroom, full warranty and a clean foundation. The practical recommendation is to retrofit first whenever the frame passes inspection, then revisit a new line only when volume growth or a new bottle format outruns the upgraded line. YuDa supports both routes, which means the same supplier can retrofit today and supply the new line tomorrow without a painful data and format break.
YuDa New-Line Specification Tables
When a retrofit is not enough, the replacement should come from a real, documented machine family. YuDa builds four PET blow product groups that map neatly onto the tiers above: the FGX high-speed series for mass beverage output, the Standard Speed full-automatic series for growing lines, the Semi-Auto series for small enterprises and ready-to-ship needs, and the blowing-filling-capping combi solutions for compact integrated plants. The tables below give typical specifications drawn from YuDa’s documented product ranges.
YuDa FGX High-Speed Series (High Speed Product Group)
The FGX series is YuDa’s high-speed automatic line, rated from 8000 to 15000 bottles per hour, built around a unique cam linking system that integrates mold-opening, mold-locking and bottom-mold-elevating in one movement and a high-speed servo driving system. Single-mode speed is in the 2500 to 3000 bottles per hour range, so multi-cavity layouts reach the top of the band. The compact 38.1 mm heater distance underpins the more than 30 percent electricity saving versus conventional heating ovens.
| Specification | FGX High-Speed (typical) |
|---|---|
| Output range | 8000 to 15000 BPH |
| Single-mode speed | 2500 to 3000 BPH per mode |
| Typical cavity number | Up to 8 cavities by configuration |
| Heater distance | 38.1 mm compact pitch |
| Energy saving versus conventional oven | More than 30 percent |
| Drive system | High-speed servo with cam linking |
| Monitoring | Remote monitoring ready |
| Best fit | High-volume beverage and water |
YuDa Standard Speed Full-Automatic Series
The Standard Speed series covers 1000 to 7000 bottles per hour with full automation, advanced heating systems and energy-saving technologies. It is the natural replacement when a Medium tier retrofit has been exhausted but volume has not yet justified the FGX high-speed band. Modular design keeps maintenance and changeovers convenient and cost-saving, which matters for plants running several bottle sizes.
| Specification | Standard Speed (typical) |
|---|---|
| Output range | 1000 to 7000 BPH |
| Typical cavity number | 2 to 6 cavities by configuration |
| Automation | Full automatic |
| Heating system | Advanced, energy-saving oven |
| Energy saving | Up to about 25 percent versus old lines |
| Design | Modular for easy changeover |
| Best fit | Growing regional bottlers |
YuDa Semi-Auto Series and Combi Solutions
The Semi-Auto series targets lower procurement cost and small enterprises, with units ready to ship. It is the entry point for workshops that cannot yet justify automation but still need reliable PET bottles. For plants that want blowing, filling and capping in one compact footprint, YuDa offers the Linear Blowing-Filling-Capping CombiBlock, a mini linear BFC that is simple, easy to operate and saves plant area, plus the Bottle Blow-Filling-Capping machine that produces PET bottles while filling drinking water and installs caps in one process. These combi solutions are especially useful when a retrofit must also shorten the line layout.
| Specification | Semi-Auto (typical) | Linear BFC CombiBlock (typical) |
|---|---|---|
| Procurement cost | Low | Medium |
| Automation level | Semi-automatic, manual load | Integrated blowing-filling-capping |
| Typical cavity number | 2 cavities common | Mini linear, compact pitch |
| Lead time | Ready to ship | Short, compact footprint |
| Plant area | Standard | Saves floor space |
| Best fit | Small enterprise, startup | Compact water filling plant |
Application Industries: Old-Line Modernization and Beverage Packaging
The low-cost transformation scheme applies across the industries that already run PET blow lines, and the two anchors are old-line modernization and beverage packaging. Old-line modernization is the umbrella goal: extending the productive life of installed assets instead of scrapping sound steel and controls. Beverage packaging is the largest end market, because water, carbonated drinks, juice and ready-to-drink tea all depend on stable, lightweight PET bottles at high volume.
Within beverage packaging, the scheme serves several concrete product types. Drinking water in 330 ml to 5 L formats drives the highest volumes and the strongest case for oven and servo retrofits, since energy and gram weight dominate cost. Carbonated beverage bottles demand precise preform temperature and blow pressure, so control and monitoring retrofits protect the pressure-resistant base design. Edible oil and condiment bottles benefit from mold and lightweighting work because wall distribution affects squeeze and shelf stability. Household care and personal care bottles gain from automation retrofits that reduce handling scuffs on cosmetic-grade surfaces.
Beyond beverages, the same retrofit logic supports edible oil, dairy, pharmaceutical and cosmetic packaging where PET has replaced glass or PVC for weight and breakage reasons. In every case the transformation starts from the same baseline measurement and the same five paths; only the bottleneck changes. A pharmaceutical line may prioritize monitoring and validation, while a water line prioritizes energy and gram weight. YuDa’s range, from Semi-Auto to FGX high-speed, means the same supplier can serve a small cosmetic bottler and a national water brand with documented models rather than custom promises. The modernization angle is especially relevant for plants that already passed a food-safety or customer audit on the existing line, because a retrofit preserves the validated layout, air handling and hygiene zones that a new line would force them to re-certify. Keeping the certified envelope intact while upgrading the dated subsystems is frequently the fastest route to a lower cost of quality.
Selection Guidance: Requirement to Recommended Model
Choosing between retrofit and new line, and then between YuDa models, is easier with a direct requirement-to-model table. The guidance below assumes the existing frame is sound; if the frame fails inspection, move one row down to the new-line option.
| Customer Requirement | Recommended Action | YuDa Model or Path |
|---|---|---|
| Old line, sound frame, need lower energy cost | Low tier retrofit | Oven upgrade plus servo retrofit |
| Old line, high labor cost, unexplained stops | Medium tier retrofit | Add take-out robot, control, remote monitoring |
| Small workshop, limited budget, startup | New entry machine | YuDa Semi-Auto series |
| Growing regional bottler, 1000 to 7000 BPH | New standard line | YuDa Standard Speed full-automatic series |
| High-volume beverage, 8000 to 15000 BPH | New high-speed line | YuDa FGX high-speed series |
| Tight floor space, water filling in one step | Combi solution | YuDa Linear BFC CombiBlock or BFC machine |
| Need lower gram weight, stable base already | High tier mold path | New blow mold plus bottle redesign |
The table is the practical bridge between the technical paths and the commercial decision. A plant that answers the first two rows is almost always a retrofit candidate and should start with the Low or Medium tier. A plant in the middle rows has outgrown its line and should buy new, choosing the YuDa model whose output band matches its forecast rather than the largest machine available. Oversizing wastes the energy index advantage, because a line running below its designed speed is itself inefficient.
Service and Support
A transformation is only as good as the support behind it, which is why YuDa, a Wanplas factory, wraps both retrofits and new lines in the Wanplas group service commitments. Before shipment every machine and retrofit kit is tested so that performance is verified, not assumed. On-site installation and commissioning are handled by engineers who also train the customer’s operators, so the upgraded line reaches rated output quickly rather than through a long trial-and-error period.
The Wanplas group policy of USD 500 free spare parts every year gives owners a predictable buffer against wear items such as heaters, seals and sensors, and damaged parts within warranty are replaced free. Remote monitoring means many faults are diagnosed before they cause a full stoppage, and the open-factory policy welcomes customers to visit, audit the build quality and witness a trial run on their own bottle format. For bottlers planning a multi-year roadmap, this continuity matters: the same supplier can retrofit today, supply a Standard Speed line next year, and add an FGX high-speed line later, all on a shared control and mold standard.
Maintenance and Operations After Transformation
A low-cost transformation changes the maintenance profile of the line. Servo systems and PLC controls fail less often than relays and pneumatics, but they need different care: clean cabinets, stable power, and firmware and recipe backups. The operations team should adopt a few habits that protect the gains.
First, keep a heater-hour log and replace lamps in matched sets so the preform temperature profile stays symmetric; uneven lamps are the fastest way to lose the energy and weight gains. Second, back up the PLC recipe for every bottle format and label it by gram weight and neck finish, so changeovers are repeatable. Third, review the remote monitoring dashboard weekly for cycle-count and reject trends, because a slow drift in reject rate is the early signal of an oven or mold issue. Fourth, schedule the USD 500 free spare parts each year for the items the log shows wearing fastest, rather than waiting for a failure. Fifth, re-measure the three baseline numbers, output, kWh per 1,000 bottles and reject rate, every quarter and compare them with the pre-transformation baseline to confirm the index improvements are holding.
Operators also need a short checklist for the new servo and robot motions: verify synchronization after any mold change, confirm the take-out grips are aligned to the new bottle pitch, and never bypass the safety interlocks added during the control retrofit. These small disciplines are what keep a Low or Medium tier project delivering its payback index point year after year instead of decaying back toward the old baseline.
Frequently Asked Questions
What is the most cost-effective first retrofit for an old PET bottle blowing production line?
For most ten-year-old lines the highest return comes from upgrading the infrared heating oven and converting the main drives to servo. Closing the heater pitch to a compact layout and replacing asynchronous motors with servo drives typically recovers the investment within a Low cost tier and reduces electricity use by a meaningful index point without touching the blow module.
Can an old one-step or two-step PET line be upgraded to full servo without replacing the blow mold?
In many cases yes. Servo retrofit kits drive the mold-opening, mold-locking and bottom-mold-elevating movements, and they can be matched to the existing blow mold cavity layout. A quick inspection of the mold clamping unit and pitch is needed before confirming, but the majority of stable molds remain usable after a control and drive upgrade.
How much energy can a retrofit save compared with a conventional old line?
Measured as an index where a ten-year-old conventional line equals 100, a heater plus servo retrofit typically lands near 70 to 75, while a high-tier modular rebuild with new molds reaches about 60 to 65. The figures are relative because absolute kWh per 1,000 bottles depends on bottle gram weight, preform temperature and ambient conditions.
Is it better to retrofit or buy a new PET blow molding machine?
Retrofit wins when the base frame, mold clamping unit and oven structure are sound and only drives, controls and heating are dated. New line purchase is better when capacity must rise by more than a tier, when bottle gram weight must drop sharply, or when the existing frame no longer meets safety and hygiene requirements. Use the cost tier table and the retrofit versus new comparison to decide.
Which YuDa model fits a small workshop with limited budget?
The YuDa Semi-Auto series is built for lower procurement cost and small enterprises, with units ready to ship. It covers low output needs and is the natural entry point before moving to the Standard Speed full-automatic series as volume grows.
What support does YuDa provide after a retrofit or new line purchase?
YuDa, a Wanplas factory, provides factory testing before shipment, on-site installation and commissioning, operator training, remote monitoring through the control system, and the Wanplas group policy of USD 500 free spare parts every year plus warranty replacement of damaged parts. Customers may also visit the factory to audit the equipment.
How long does a Low or Medium tier retrofit take on the production floor?
A Low tier heater and servo package is often installed during a planned weekend stoppage with limited downtime. A Medium tier that adds a take-out robot, full control replacement and remote monitoring usually needs a one to two week window, partially overlapping with normal maintenance so daily output loss stays controlled.
Conclusion
A low-cost transformation scheme for an old PET bottle blowing production line is not a single purchase but a sequenced set of upgrades aimed at the five subsystems that actually cost money: take-out robot, heating oven, servo drive, electrical control and blow mold. By measuring output, energy and reject rate first, then placing each upgrade in a Low, Medium or High cost tier defined by percentage share and payback index points, a plant can recover most of a new line’s performance at a fraction of the capital. The energy table shows why a Low tier retrofit already captures roughly two-thirds of the gap to a new high-speed line, while the retrofit versus new comparison shows when a full replacement finally makes sense.
YuDa, a Wanplas factory with more than 20 years of PET blow molding experience, 60-plus countries served, top two status in China and 20-plus patents, supplies both the retrofit modules and the replacement machines from one document-backed range: the FGX high-speed series, the Standard Speed full-automatic series, the Semi-Auto series and the blowing-filling-capping combi solutions. Send your current line model, bottle format, output target and energy data, and the engineering team will propose a phased transformation that matches your cost tier and capacity roadmap, then support it with factory testing, on-site commissioning, remote monitoring and the Wanplas group commitment of USD 500 free spare parts every year. A well-planned retrofit today keeps your line competitive; a clear new-line path tomorrow keeps your growth unblocked.






